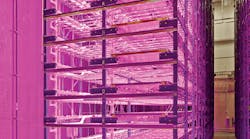
How do you fit 2.2 million plants into one plant? At the iBio plant in College Station, Texas, living plants are used as bioreactors to produce vaccine-grade protein.
“We grow 330,000 kg of plants in one year,” said Barry Holtz, president of iBio, who spoke at the Rockwell Automation Process Solutions User Group (PSUG) 2017 this week in Houston. The biopharmaceutical company’s facility is more than 100,000 sq ft, stands more than five stories high and sits on a 21-acre site. “We have unidirectional flow in the building,” explained Holtz. “Everything is automated that can be automated—we don’t allow people to touch our plants.”
The iBio Vertical Pharming manufacturing process, which is automated largely by Rockwell Automation control systems, involves three steps—plant production, plant infiltration and downstream purification in autonomous cleanrooms.
[sidebar id =1]
The protein-making capabilities of vacuum-infiltrated Nicotiana benthamiana, relative of an Australian tobacco plant grown in a hydroponic system, are hijacked, so the plant’s leaves become bioreactors.
“We seed 1,200 plants per tray, and then we go into germination,” Holtz said. The 55-ft-high laminar air-flow room where germination takes place was designed using computational flow dynamics, and temperature-controlled within 2 °F. The second, larger growth room stands 14 layers high with a capacity of 1.2 million plants. When the plants reach 8-10 g, they are the perfect size to be bioreactors.
“Agroinfiltration is where the magic happens,” said Holtz. “It’s where we infect the plant with the vector for a transient expression of new protein.” The plants are placed upside down in an infecting liquid, evacuated to 1/3 of atmosphere, and brought back to atmospheric. “All of their protein-synthesizing DNA is hijacked,” he said.
Once the plants are fully grown, their proteins are extracted in clean rooms using processes familiar to any biopharmaceutical operation. Seven autonomous clean rooms, or portable pods, are fitted with air bearings so they can be lifted an inch off the floor and moved with one hand. “Each clean room has 100% redundancy, and it’s all controlled by ControlLogix. We even have our own fire suppression in these rooms,” Holtz said. The process is managed with a PlantPAx distributed control system.
From start to future
The process was originally developed in a challenge from the Defense Advanced Research Projects Agency (DARPA). “Our first challenge was to design a commercial biotherapeutics facility using a plant-made pharmaceutical platform, and design the facility to be hardened, self-sufficient and have high containment,” explained Holtz. “The test was that DARPA sent us a gene sequence by email, then we had to make 50 million doses in 12 weeks, because that’s what stops a pandemic in America.”
The support structure for the building is enormous. “We started Quality by Design at the start. We computer-optimized all of the drawings,” said Holtz. “The building was built in 3D CAD before we poured any concrete. We use a series of design tools in the Destini Profiler software system. It uses a parametric database, so we can move walls and watch the capex change. To build ours, we raised the first wall on June 8, 2010, and we moved in on March 22, 2011, less than a year later.
“We used some very advanced techniques. And now, we’re currently working in Brazil and South Africa to transfer this technology to other countries.”
In the pharmaceutical industry, the final customer is the patient, explained Holtz. “Screwing up is not allowed,” he said. “We have to be 100% correct each time, which is a daunting task. Quality by Design includes assessment, quality target product profile, risk analysis, process development and validation. I think facility design, information management and automation should be attacked at every step. We are one of the, if not the, most regulated industry on the planet. We’re thinking inside the box. We must have a constantly improvable environment.
“Improvement should be iterative, not retrospective.” For iBio, that means starting with baseline equipment and software, then improving on it. With the initial layers of automation already in place, the next step will be to add the manufacturing execution system (MES) to the top layer. “We just completed a new front-end engineering design (FEED) study,” he explained. “We’ve had as many as 13 people around the table working on this. We’re going to take this FEED study and build toward a full MES.”
Holtz said iBio has identified six expectations of an automation supplier:
- Collaborative development environment, which means exceptional people;
- Genuine understanding of iBio technology;
- Multiple levels of service;
- Global service model, with troubleshooting 24/7;
- Long-term dedication to the pharma/biotech industry; and,
- New robust products and the maintenance of legacy products.
These expectations are met by Rockwell Automation, Holtz said.
About the Author
Mike Bacidore
Mike Bacidore
 Leaders Logo
Leaders relevant to this article: